

A printed paper facing can look sound when it leaves a press, yet curl or separate during storage. A delicate fabric can remain firmly bonded while losing the soft feel that made it worth buying. For businesses considering EVA hot melt adhesive, avoiding heat damage and obtaining acceptable service durability are related decisions. Neither follows automatically from a low processing temperature.
Vinyl-acetate content, film thickness and the actual surfaces being joined all belong in that decision. The commercial argument for an EVA film is strongest when it solves an area-bonding problem without imposing a service requirement the chosen formulation cannot meet. Buyers therefore need to consider the finished package or textile article before comparing adhesive prices. Low-temperature assembly is useful only if the resulting product remains fit for its intended job.
Choose the adhesive form before choosing a lower temperature
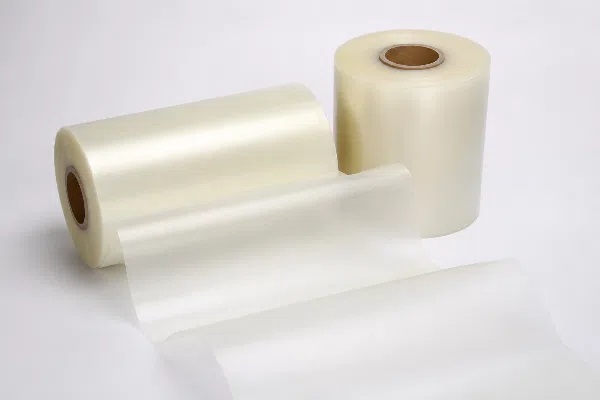
Teng Yang’s EVA product page distinguishes continuous film for area lamination from pellets for molten dispensing, powder for scatter coating and open web for lighter, more permeable constructions. These forms place adhesive differently. A paper-to-fabric laminate may suit a film laid between the surfaces, whereas a packaging machine that applies narrow beads needs a compatible dispensing material rather than a roll of film.
Format comes first. Even when the purchasing description says only “hot melt adhesive,” replacing a bead with a continuous layer changes bonded area, material use, the way the assembly bends and the equipment required to place and activate the adhesive reliably. Start with the intended bond geometry and the available production method; otherwise, a discussion about low-temperature chemistry can conceal a basic mismatch between the supplied form and the line.
Where it stops: film is not a direct refill for a glue tank. A shared polymer name does not make the formats interchangeable.
Prevent heat damage at the finished surface
Henkel’s commercial overview of packaging adhesives explains that thermoplastic hot melts soften with heating and discusses lower-temperature application for heat-sensitive substrates. That is general category context from another supplier, not evidence of the performance of a particular EVA film.
Converters need enough heat to reach the adhesive before the printed face, foam backing or fabric finish changes. Watch the entire construction. An undamaged outer face does not establish that the hidden bond line received adequate heat, and a strong initial bond does not excuse flattened foam or a stiffened textile. Evaluate appearance, handling and adhesion together after cooling, using the material combination that customers will receive.
Ask the film supplier for starting conditions suitable for that combination, then check them on the intended equipment. Lowering a controller setting without examining bond development can merely exchange visible damage for a less visible adhesion problem.
Use vinyl-acetate content to discuss grades, not to predict a lifetime
Teng Yang gives 18–40% vinyl-acetate content as a representative industry range, explicitly not a Teng Yang test certificate. Its page describes vinyl-acetate content as a formulation variable affecting polarity and crystallinity, alongside other ingredients that influence tack, melt flow and setting behavior.
This helps explain why “EVA” is an incomplete specification. A buyer selecting a laminating adhesive should identify a grade and ask how its formulation suits the proposed surfaces, rather than assuming a higher vinyl-acetate figure improves every property at once. Composition can guide the conversation; it cannot replace a bond trial or a documented service limit.
When reviewing Teng Yang’s EVA hot melt adhesive film, use the published material discussion to prepare that grade-level enquiry. Request the current data associated with the sample being supplied. A broad reference range cannot tell a purchasing team whether an unnamed roll will tolerate its particular storage, flexing or cleaning conditions.
Separate a heat activated adhesive from a heat-resistant bond
The website’s low-melt reference row lists a softening point of approximately 60–80°C and a press activation range of approximately 90–110°C. These are representative industry figures for discussion, not certified processing instructions or guaranteed service temperatures for an order.
The distinction is commercially important. Processing concerns making contact and forming the bond; service concerns retaining the joined shape under the conditions encountered later. A laminate can survive a brief manufacturing exposure yet move under a sustained load in a warm environment. Conversely, adopting a nominally higher-temperature grade is unhelpful if the face material is damaged before that grade bonds properly.
Describe the likely heat exposure and loading to the supplier separately from the proposed press conditions. For a package, that might include warm storage with stressed folds. For a textile, it may include heat during care. If these uses conflict with the grade’s demonstrated capability, changing the adhesive family or the construction deserves consideration.
Keep packaging claims tied to the actual application
Packaging is not a single exposure category. An outer decorative sleeve, an internal divider and a layer close to food have different obligations, even when all use paper. The buyer should state the intended contact, the other layers and the destination market before asking whether an adhesive is suitable. A general packaging application on a supplier website cannot settle those details.
Food-related uses require documentation for the identified grade and intended construction, requested through the responsible compliance team. Do not transfer a competing manufacturer’s food-packaging claims to EVA as a whole, or treat the absence of solvent in a film as proof of food-contact suitability. Those are different questions.
Keep the purchasing description consistent with the evidence received. If the supplier has supplied a sample for a non-contact decorative layer, the resulting approval should say so. Expanding its use later requires examining the new application, rather than relying on the old sample’s acceptable appearance.
Make fabric adhesive selection include touch, stretch and care
The EVA page identifies washing, sustained heat loading and contact with plasticised materials as conditions requiring attention, and offers both release paper and bare-film formats for buyers whose placement methods differ even when they are investigating the same basic adhesive chemistry. Successful placement is only the start. The fabric must still behave as the finished article requires.
Film thickness should therefore be considered alongside handle and adhesive coverage. A continuous layer that feels acceptable in a flat swatch may make a folded or stretched assembly unpleasantly rigid. Evaluate the intended seam or bonded area in its working shape, including the cleaning instructions that will accompany the product.
Stretch apparel calls for a fabric adhesive assessed for recovery after deformation as well as initial attachment. Heavy laundering or elastic recovery may justify evaluating another adhesive chemistry. That is an application decision supported by comparative samples, not evidence that every EVA grade fails or that every alternative passes.
Check service durability without disguising it as a savings claim
Low-temperature processing often attracts attention because a business hopes to reduce waste or operating costs. Neither benefit is automatic. A slower cycle, extra handling or more rejected assemblies can alter the commercial result, while the energy comparison depends on the equipment, its operating schedule and the amount of acceptable output produced under the conditions being compared. Measure the production change before advertising it.
For the laminate itself, define what must remain acceptable after the expected exposure: edges must stay attached, printed surfaces must remain presentable and the article must retain its intended function. Compare exposed samples with retained controls. Record what changed and where, rather than reducing every observation to a vague “bond passed.”
Be careful with accelerated screening. A useful comparison between candidates does not automatically establish a calendar lifetime. Explain the conditions actually examined, keep the limitations attached to the result and avoid presenting a laboratory exercise as evidence of field returns that have not been observed.
Order against an accepted construction
A useful enquiry describes the mating surfaces, adhesive form, film thickness, placement method, equipment and service exposure. Include finished samples or representative materials where possible, especially when coatings and textile finishes affect the bonding face. Ask the supplier to identify the proposed grade and explain any conditions outside its recommended use.
Before approving volume, agree which cooled appearance and exposed-bond results define acceptance. Retain the accepted construction and its processing record so that a later change of paper coating, foam backing or fabric finish triggers a meaningful review. The same adhesive can face a different task when its neighbouring materials change.
EVA earns its place when low-temperature area bonding and the intended service conditions fit the same grade. If they do not, the sensible commercial response is to revise the material choice before the mismatch reaches customers. A cheaper roll is of little value when it cannot produce the specified finished article.